Checklist: Verifying Coating Thickness on Incoming Parts
This guide provides a step-by-step method for verifying coating thickness on incoming parts. It covers measurement methods, documentation checks, and red flags to identify nonconforming coatings before acceptance, ensuring supplier compliance and protecting your quality standards.
- Verify coating thickness using calibrated instruments that match the coating type and substrate
- Cross-reference measured values against the original specification and drawing callouts
- Check supplier certificates of analysis and traceability documents against your incoming inspection records
- Flag parts where thickness variation exceeds tolerance or where surface defects are visible
- Maintain a documented log of all verification activities for audit and continuous improvement purposes
Why Coating Thickness Verification Matters for Incoming Parts
Coating thickness directly affects corrosion resistance, wear performance, and dimensional fit. When incoming parts fail to meet the specified thickness, downstream processes can suffer from premature failure, rework, or line stoppages. A structured verification process catches these issues at the receiving dock, not after assembly.
This checklist is designed for quality engineers, receiving inspectors, and procurement teams who need a repeatable method to confirm that delivered parts match the contractual specification. It applies to electroplated, anodized, and chemically converted coatings on steel, aluminum, and other base metals.
Pre-Inspection: Confirming Documents and Specifications
Before touching a single part, verify that the paperwork matches the purchase order. The supplier should provide a certificate of analysis or test report that lists the coating process, thickness specifications, and measured values.
Check the following items:
- Does the certificate of analysis reference the correct part number and drawing revision?
- Does the specified thickness range match the engineering drawing callout?
- Is the coating process clearly identified (e.g., nickel plating, chromate conversion, anodizing)?
- Are the measurement points and method described on the report?
- Does the report include the lot or batch number for traceability?
If the documentation is incomplete or ambiguous, hold the shipment for clarification. Do not proceed to physical inspection until the paper trail is clean. Missing or mismatched documents are a common indicator of poor supplier quality control and can signal systemic issues with the coating operation.
Selecting the Right Measurement Instrument
The measurement method must be appropriate for the coating type and substrate material. Different coatings require different tools, and using the wrong instrument produces unreliable data.
| Coating Type | Recommended Instrument | Typical Measurement Principle |
|---|---|---|
| Electroplated metals | X-ray fluorescence thickness gauge | Non-destructive beam interaction |
| Anodized aluminum | Eddy current gauge or cross-section | Inductive or physical |
| Chemically converted films | Eddy current or optical | Inductive or visual |
| Thick plated parts | Micrometer or profile gauge | Contact measurement |
X-ray fluorescence gauges are the standard for most electroplated parts because they are fast and non-destructive. Eddy current instruments work well on non-conductive or semi-conductive coatings. For very thick deposits or parts with complex geometry, a cross-section method may be required.
Verify that the instrument is within calibration due date before starting the inspection. A gauge that is out of calibration can produce readings that appear correct but are systematically off. Check the calibration sticker and confirm the last calibration date against your calibration schedule.
Setting Up the Measurement Plan
A random sampling approach is insufficient for high-risk coatings. Establish a measurement plan before you begin testing.
- Identify the critical zones on each part where thickness is most likely to vary.
- Determine the minimum number of measurement points per part based on the coating specification.
- Define the acceptance criteria. Most specifications require a minimum thickness at every point and an average thickness across the sample.
- Record the measurement location on a sketch or photograph of the part.
For example, a nickel-plated fastener might require three measurements on the shank, two on the head, and one on the threads. The specification might state a minimum of 2.5 microns per point and an average of 3.0 microns across all six points. If any single point reads below 2.5 microns, the part fails, even if the average is acceptable.
Document the measurement plan in the inspection report so that the process is reproducible. If another inspector reviews the record later, they should be able to understand exactly where and how the parts were measured.
Performing the Physical Measurement
Place the instrument on the part surface and take readings at each defined point. For X-ray fluorescence gauges, ensure the surface is clean and free of oil, dirt, or oxide scale. Contaminants on the surface can scatter the beam and produce inaccurate readings.
For eddy current instruments, calibrate the gauge against a standard sample of the same coating type and substrate. Many gauges require a zero adjustment for each different part shape and material. If you are measuring aluminum anodizing on a steel substrate, the calibration must account for the difference in magnetic properties.
Record each reading immediately. Do not rely on memory. Write down the value, the location, and the instrument serial number. If you are using a handheld gauge with data logging, export the file to a secure folder and rename it with the lot number and date.
Take at least three readings at each location to account for instrument drift or surface irregularity. Report the average of the three if the specification allows, or report the lowest value if the specification requires a minimum at every point.
Evaluating Surface Condition and Defects
Thickness is only one dimension of coating quality. A part can meet the thickness specification and still fail because of surface defects. Inspect the coating visually and, if necessary, with magnification.
Look for these common defects:
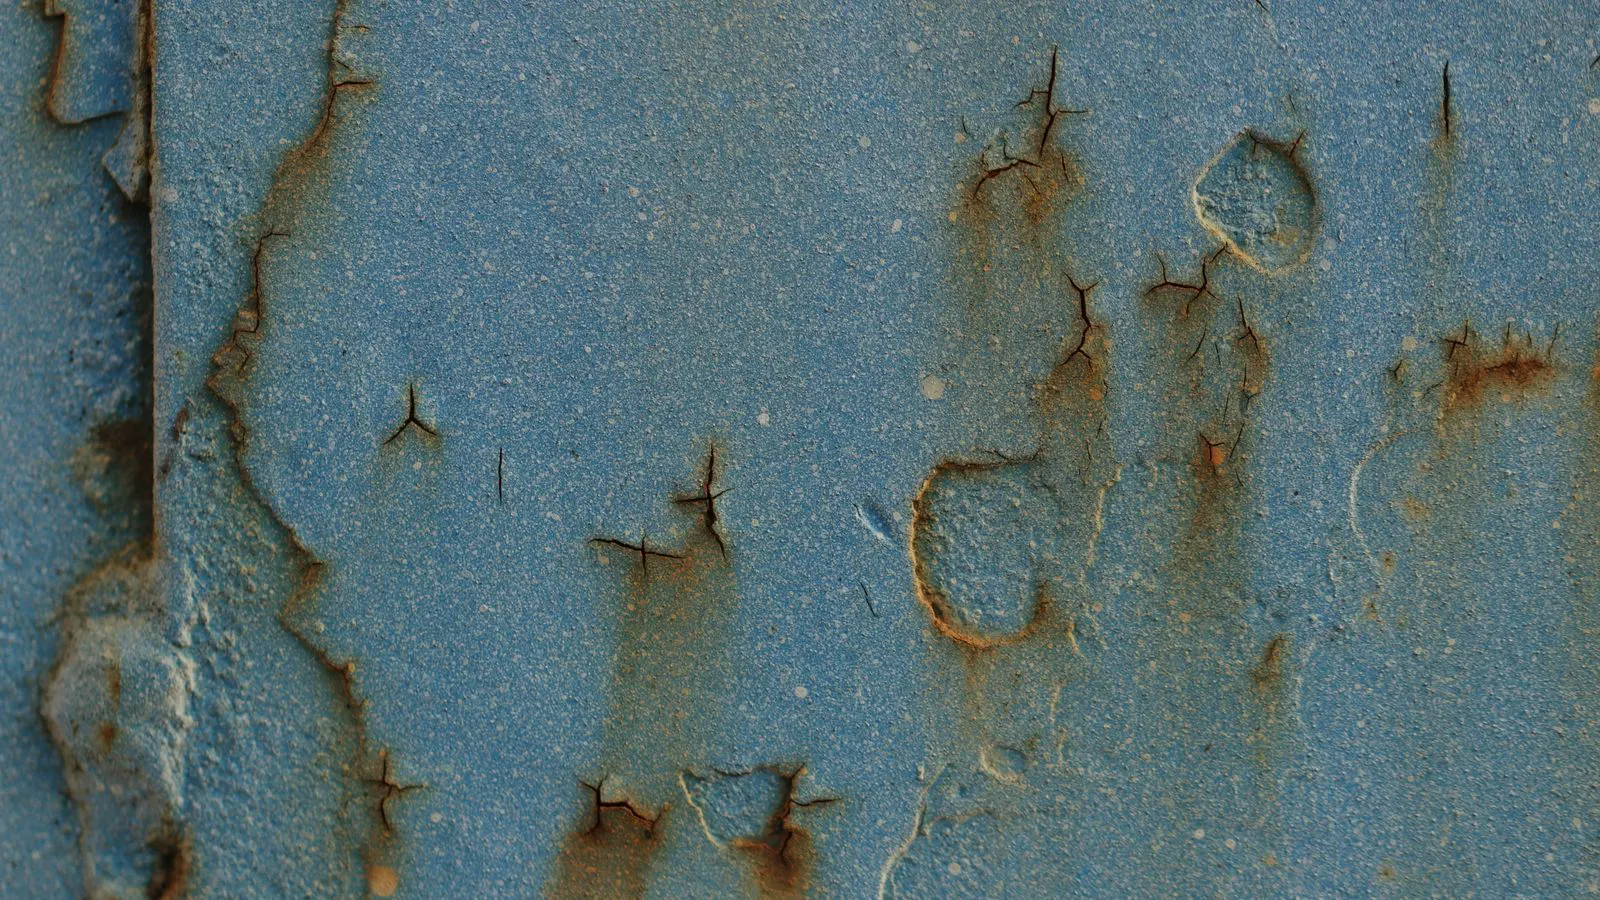
- Blistering or bubbling, which indicates adhesion failure or contamination during plating
- Pitting or porosity, which creates weak points in the coating
- Color variation or streaking, which suggests uneven deposition
- Edge build-up or thinning, which is common on sharp corners and fillets
- Stripping or flaking, which indicates poor adhesion to the substrate
A coating that is thick but blistered will fail faster than a coating that is thin but uniform. The blistered coating provides no meaningful protection because the substrate is exposed at the blister boundaries.
If you find defects, photograph them with a scale reference and note their location. Attach the photos to the inspection report. Defect location matters because it can indicate a process problem with the supplier. For example, blistering on one side of a part may point to a rinse problem, while pitting on all sides may indicate aggressive bath chemistry.
Reviewing Supplier Compliance and Traceability
Supplier compliance extends beyond the physical part. The supplier should be able to demonstrate that the coating process was controlled and that the materials used met specification.
Request the following documentation:
- Process control records showing bath chemistry, temperature, and current density during the coating run
- Raw material certificates for the plating bath chemicals
- Operator sign-off for the coating operation
- Final inspection records from the supplier’s quality department
If the supplier cannot provide these records, treat it as a compliance gap. A supplier that cannot trace its coating process to the specific lot of chemicals used cannot be expected to maintain consistent quality over time.
Cross-reference the supplier’s test report with your own measurement results. If your readings are consistently below the supplier’s reported values, there is a discrepancy that needs investigation. The discrepancy could be due to measurement method differences, instrument calibration drift, or actual nonconforming parts.
Documenting and Disposing of Nonconforming Parts
When a part fails the coating thickness verification, isolate it from the conforming stock immediately. Mark the part with a nonconforming label and place it in a designated quarantine area.
Document the failure in the inspection report. Include the part number, lot number, measurement values, and a description of any visible defects. Attach the calibration certificate for the instrument used and the supplier’s certificate of analysis.
Notify the supplier and your quality engineer before dispositioning the part. The supplier may offer a credit, rework, or replacement. You may also need to determine whether the failure is a one-off event or part of a broader lot problem. If multiple parts from the same lot fail, hold the entire lot pending review.
Keep the nonconforming part and all associated records for the duration of your quality retention period. These records may be needed for customer claims, warranty disputes, or internal quality improvement projects.
Maintaining the Verification System Over Time
A one-time verification is not enough. The measurement process and instrument calibration must be maintained on a schedule.
- Calibrate all thickness gauges at least annually, or more frequently if the gauge is used heavily or in a harsh environment.
- Re-verify the measurement plan when the part design changes or when a new supplier is introduced.
- Review the inspection records quarterly to identify trends. Are certain lots consistently near the lower specification limit? Are defects recurring?
- Update supplier scorecards based on coating compliance performance.
If you notice a trend of parts arriving near the lower thickness limit, raise the issue with the supplier during a quality review. Early intervention prevents larger failures and strengthens the supplier relationship.
The goal of this checklist is not to create bureaucracy. It is to create a reliable, defensible record that incoming parts meet the specification. When a failure occurs, you want to be able to point to a clear process that caught the problem and documented it. That record protects your product, your customers, and your reputation.
Frequently asked questions
What is the minimum number of measurement points required for coating thickness verification?
The number depends on the part size, complexity, and the specification. Most engineering drawings call for a specific number of points per part, often three to six per critical zone. Always follow the drawing callout.
Can I use a micrometer to measure an electroplated coating on a small part?
Micrometers are generally not suitable for thin electroplated coatings because the contact pressure can compress the coating or damage the surface. Use a non-destructive method such as X-ray fluorescence or eddy current for thin films.
What should I do if the supplier's certificate of analysis does not match my measurement results?
Hold the shipment and contact the supplier for clarification. Compare the measurement methods used by both parties. If the discrepancy persists, escalate the issue for a formal quality review.
How often should I calibrate my coating thickness gauge?
Calibrate at least annually, or more frequently if the gauge is used daily or in a corrosive environment. Follow the manufacturer's recommended interval and your internal calibration schedule.
Is a coating that meets the average thickness but fails at one point acceptable?
No. Most specifications require a minimum thickness at every measured point. A single point below the minimum is a failure, even if the average is within specification.