Outlook: Automated Passivation in High-Volume Manufacturing
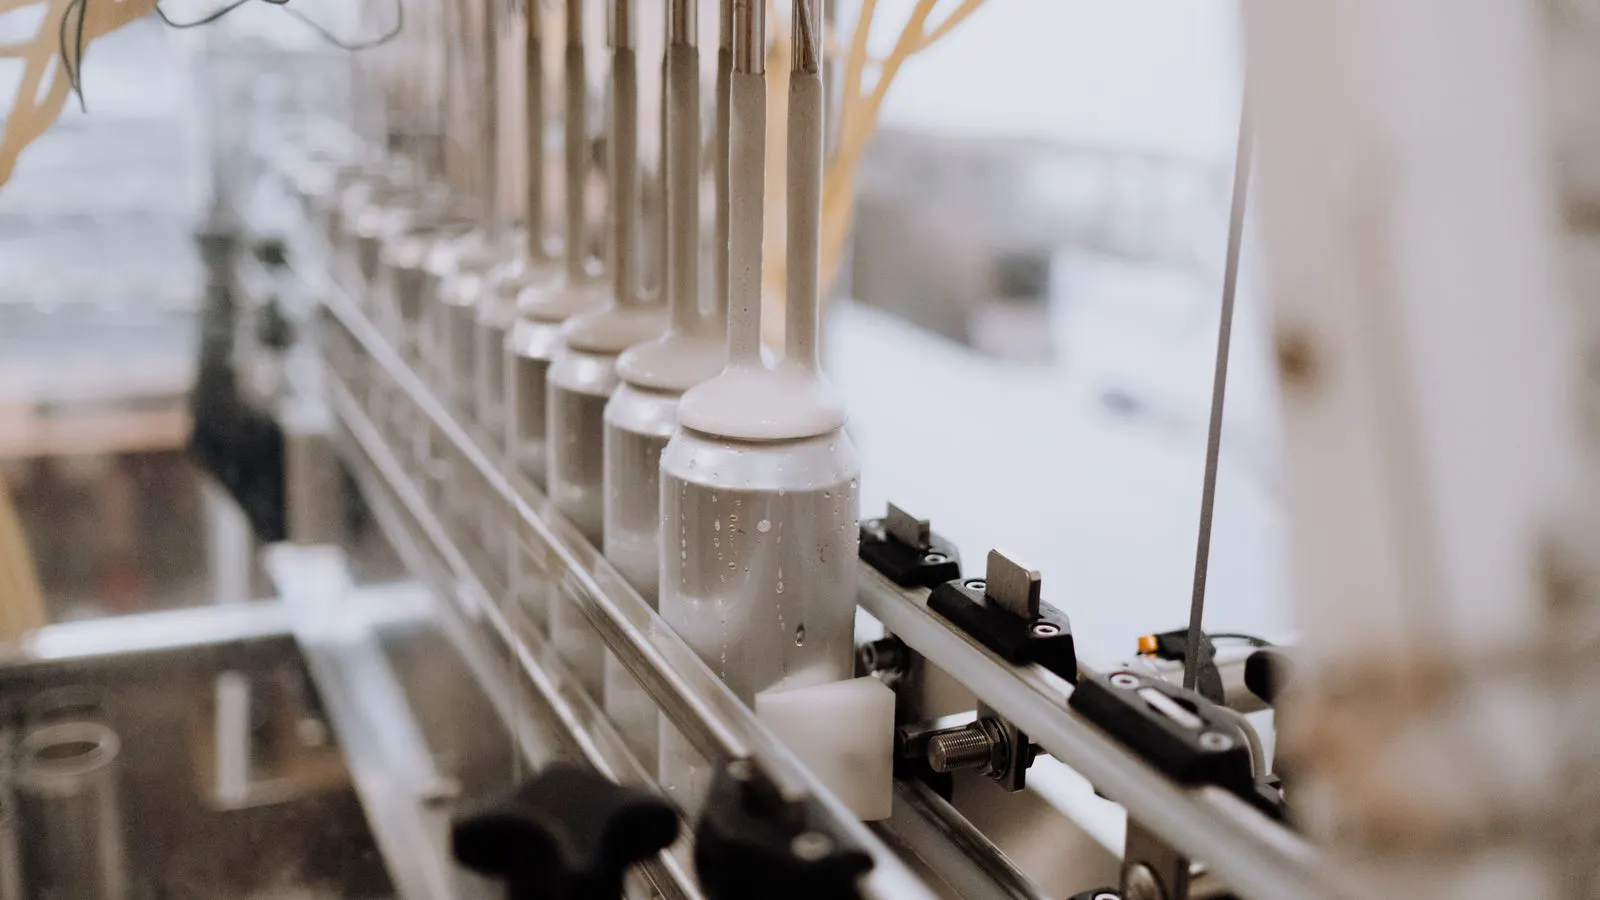
Automated passivation trends shift high volume finishing from batch processing to continuous, data-driven lines. Buyers should plan for tighter QC, better throughput, and integrated compliance tracking. Preparation requires vendor evaluation, line integration, and staff retraining.
- Automation moves passivation from manual batches to continuous high speed lines, improving throughput and consistency.
- Integrated sensors and data capture make compliance verification and traceability easier for imported and domestic parts.
- Buyers should evaluate vendors on line integration, maintenance access, and the ability to handle mixed material lots.
- Staff roles shift from chemical handling to monitoring, data review, and exception management.
- Preparation requires pilot runs, clear acceptance criteria, and a plan for handling mixed stainless grades and tolerances.
How automation changes passivation throughput
High volume finishing lines are moving away from manual batch handling. Parts that once waited in trays for a chemist to load, rinse, and inspect now move through automated conveyors, racks, or pallets. This shift changes the economics of passivation. A single operator can oversee multiple racks instead of loading and unloading each tray by hand. The result is higher capacity without a proportional increase in headcount.
The change is most visible on stainless steel hardware lines. Think of fasteners, brackets, valve bodies, and medical components. In a manual setup, a technician lifts a rack of parts, lowers it into the tank, waits for the cycle, lifts it again, and sends it to the next stage. In an automated setup, a robotic arm or a conveyor transfers the rack. The cycle time is fixed. The operator monitors the line from a control station.
This does not mean every plant is fully automated. Many facilities use a hybrid approach. Parts are loaded onto automated racks by hand, and the racks then move through the passivation and rinse stations automatically. This hybrid model is common in medium size facilities. It captures much of the throughput benefit while keeping the initial investment lower.
The buyer perspective is clear. If your volume grows, manual passivation becomes a bottleneck. The chemist becomes the constraint. If you rely on a third party service, their manual capacity may limit their lead time. Automation changes the math. It allows a vendor to promise shorter lead times for larger volumes. It also allows an in house plant to scale output without building a larger chemical room.
What changes in quality control
Automation does not just move parts faster. It also changes how quality is measured. In a manual line, QC is often a sampling exercise. A technician pulls a few parts after the cycle. They inspect for color, film formation, and visible defects. They may run a spot check with a wet film test. This works for small batches. It becomes harder to defend for high volume lots.
An automated line can capture data at every station. A camera system checks for visible defects as parts move through the line. A sensor checks rinse water quality. A conductivity meter confirms tank chemistry. The data is tied to the batch number. If a lot fails, the plant can trace the problem back to a specific tank, a specific time window, or a specific chemical lot.
This traceability matters for imported parts and regulated industries. If a valve body passes an internal check but fails a customer salt spray test, the plant needs to show that the passivation process was correct at the time of manufacture. Automated logging makes that easier. The plant can export a report showing tank temperature, chemistry levels, cycle time, and rinse quality for the exact batch.
For buyers, this changes the acceptance criteria. You can move from visual inspection to data review. Instead of asking a vendor to show you a wet film test, you can ask for the process data. You can define pass as a range of sensor readings, not just a color match. You can require that the vendor retains the data for a defined period.
Capacity planning shifts
When you plan for passivation, you must now account for line design, not just tank volume. In a manual setup, capacity is driven by tank size and cycle time. If you need more volume, you add another tank or run more shifts. In an automated setup, capacity is limited by the conveyor speed, the rack size, the transfer time, and the number of parallel lines.
This means the capacity conversation changes. You are no longer just asking how many parts a tank can hold. You are asking how many racks the line can process per hour. You are asking if the line can handle mixed material lots. You are asking if the line can run unattended for a full shift.
The mixed material question is common. A hardware plant may passivate 304, 316, and 430 stainless in the same facility. Each grade has different passivation requirements. 316 may need a different chemical concentration than 304. 430 may need a different cycle time. An automated line must be programmed to handle these differences. If the line is a single tank setup, it may not be able to switch chemistries quickly. If it has multiple tanks and a programmable transfer system, it can.
Buyers should ask vendors how they handle mixed grades. Do they segregate lots by grade? Do they use separate tanks for different chemistries? Do they flush the line between lots? Do they use a software system to track which tank handled which grade? These details matter. A line that cannot handle mixed grades may force you to split your lots. Splitting lots increases handling, increases QC cost, and can slow delivery.
Maintenance and chemical handling
Automation introduces maintenance complexity. A manual line has a few moving parts. A pump, a tank, a rack, and maybe a conveyor. An automated line has sensors, actuators, control valves, and a control system. If a sensor fails, the line may stop. If a valve fails, the chemistry may be off. If the control system has a software glitch, the line may not start.
This changes the maintenance model. You need a plan for preventive maintenance. You need a plan for emergency response. You need to know who is responsible for repairs. If the line is vendor operated, the vendor must have a service contract. If the line is in house, you need a maintenance contract with the equipment supplier.
Chemical handling also changes. In a manual line, a chemist checks the tank by sampling. In an automated line, sensors check the tank continuously. But sensors can drift. They need calibration. The chemist still has a role, but the role changes. The chemist becomes a data reviewer. They check the sensor trends. They compare the data to the process window. They intervene when the data goes out of range.
This is a good thing. It reduces the risk of a bad lot passing because a human missed a sample. It also reduces the risk of over adding chemicals. In a manual setup, a chemist may add too much acid because the color looks off. In an automated setup, the control system adds acid based on conductivity and pH readings. The result is a tighter process.
Staff roles and training
The people who run the line change roles. A passivation technician who once loaded trays and checked tanks now monitors a screen. They watch the process data. They check the alarms. They handle exceptions. They may still do a visual check at the end of the line, but they do it on a sample, not on every part.
This shift requires training. The technician must understand the process data. They must know what a normal trend looks like. They must know when to call maintenance. They must know how to interpret a sensor reading. They must know the acceptance criteria for the parts.
The buyer should ask about the training plan. If you are buying a line, the vendor should provide training. If you are hiring a vendor, the vendor should show you their training records. The people who run the line must understand the process. If they only know how to press a start button, the line will fail.
How to prepare for automated passivation
If you are planning to move to automated passivation, start with a pilot. Do not commit to a full line upgrade without a test run. Run a small lot through the new setup. Measure the results. Compare the data to your current process. Check the QC reports. Review the maintenance logs.
Define your acceptance criteria before the pilot. You need to know what pass looks like. You need to know what data you require. You need to know how long you need to retain the data. You need to know how you will handle a failed lot.
Evaluate your vendors carefully. Look at their line integration. Look at their QC capabilities. Look at their maintenance plan. Look at their ability to handle mixed material lots. Look at their training program. A vendor that can run the line is not enough. The vendor must be able to prove the process.
What to expect in the next few years
The direction is clear. More facilities will move to automated passivation. More vendors will offer data driven QC. More buyers will require process data as part of acceptance. The line between passivation and coating is blurring. Some lines will handle passivation, coating, and inspection in one integrated system.
This integration will change the way you plan. You will not order passivation separately. You will order a surface finish package that includes passivation, coating, and testing. The data will tie all three together. This is a good thing. It reduces handling. It reduces risk. It makes compliance easier.
The buyer who prepares now will be in a better position. They will have the data. They will have the process. They will have the traceability. They will not be stuck with a manual line that cannot scale. They will not be stuck with a vendor that cannot prove the process. They will have a clear path to high volume finishing with the quality control that modern manufacturing requires.
Frequently asked questions
Can automated passivation handle mixed stainless grades?
Yes, but it depends on the line design. A line with separate tanks and programmable transfer can handle mixed grades. A single tank line may not.
How does automation change QC for passivation?
Automation adds sensor data and camera checks. QC shifts from visual sampling to data review. The plant can trace a lot to specific tank readings and cycle times.
What is the main maintenance concern with automated passivation?
Sensor calibration and control system reliability. A manual line has fewer electronic components. An automated line needs a preventive maintenance plan and a service contract.
How should a buyer prepare for automated passivation?
Run a pilot. Define acceptance criteria. Require process data. Evaluate the vendor's line integration, QC, and maintenance plan.
Does automation reduce the need for a passivation chemist?
No, but it changes the role. The chemist becomes a data reviewer. They monitor trends, calibrate sensors, and intervene when data goes out of range.


