Checklist: Pre-Shipment Inspection for Plated Parts
A pre-shipment inspection of plated parts requires checking visual appearance, thickness, adhesion, and documentation. This checklist helps buyers identify defects early and enforce vendor acceptance criteria to reduce costly rework and field failures.
- Inspect plated parts for visual defects, dimensional changes, and substrate exposure before signing off on a shipment.
- Verify that the vendor has recorded thickness, adhesion, and salt spray results that match your purchase order.
- Use a standardized plating inspection form to make acceptance decisions objective and defensible.
- Check packaging and corrosion protection, as improper handling during transit can ruin a finished part.
- Document every defect clearly with photos and part numbers to support claims or rework requests.
Why a pre-shipment plating inspection matters
Plating changes the surface of a metal part, but it does not fix poor machining or weak design. A finished part can still fail if the substrate was contaminated, the geometry was wrong, or the vendor skipped a critical step. Buyers often discover these problems only after parts arrive at the plant, and by then the cost of sorting, rework, or replacement has already taken hold.
A structured plating inspection reduces risk. It gives you a repeatable way to check the part against your purchase order before you accept it. It also creates a paper trail that protects you in disputes with the vendor. The goal is simple. Confirm that the part is what you ordered, that it meets the agreed acceptance criteria, and that it will perform in the field.
The checks below are grouped by theme. Each item includes a short explanation and a red flag to watch for. Use the list as is, or adapt it to your specific application.
Visual appearance and surface condition
Start with the most obvious checks. Lay the parts on a clean, light-colored surface and inspect them under bright, diffuse light. Look for scratches, dents, pits, and discoloration. Compare the finish to an approved sample if you have one. A consistent color and texture are normal. Variation from part to part, or within a single part, is a warning sign.
Check the edges and corners first. These areas are prone to edge burn, where the plating is too thick and brittle. They are also where the substrate is most likely to be exposed if the process was not controlled. Run a soft finger, not a bare nail, along the edges to feel for sharpness or roughness.
Red flags:
- Dark or black spots that do not match the approved finish.
- Hazy or uneven color, especially after cleaning.
- Visible machining marks that should have been covered by the plating.
- Edge burn or raised, brittle edges.
- Substrate showing through in recesses or corners.
Thickness and dimensional checks
Plating adds material to the part. That material changes the dimensions. For small parts, the change may be negligible. For larger parts or thicker platings, it can affect fit and function. Your purchase order should state the required thickness and any tolerance for dimensional change. If it does not, ask the vendor to confirm the as-received thickness.
Use a micrometer to measure the part before and after plating, if you have the tooling. If not, trust the vendor’s certificate but cross-check it against the part number and lot. A certificate that is vague, missing, or does not match the shipment is a problem.
Red flags:
- Thickness outside the specified range.
- No certificate or a certificate that does not match the part number.
- Dimensional change that affects fit, such as a pin that no longer goes through a hole.
Adhesion and mechanical integrity
Plating must stick to the substrate. If it does not, it will flake, peel, or chip in service. A quick adhesion check can save you from a larger failure. For small parts, you can try a gentle scratch test with a razor blade or a dedicated adhesion tester. For larger or more critical parts, request the vendor’s test data, such as a cross-cut or pull-off test.
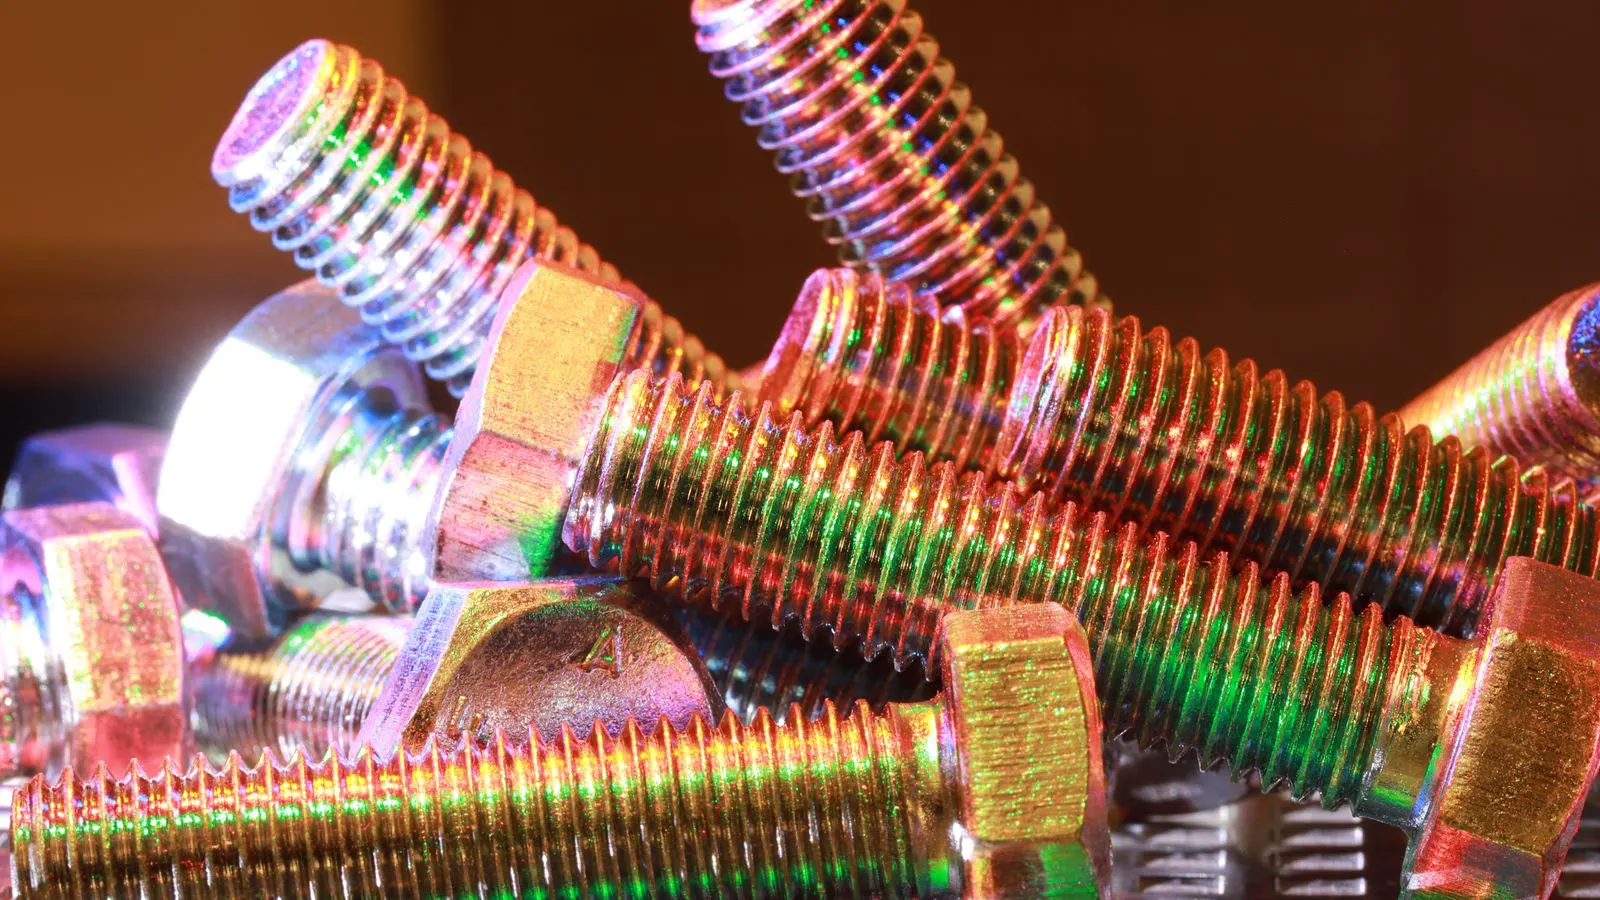
If you are receiving fasteners, check the threads. The plating must not be too thick in the thread area, or the threads will be damaged. If the plating is too thin, the threads will corrode quickly.
Red flags:
- Plating that flakes or peels when you lightly scratch it.
- No adhesion test data for critical parts.
- Plating that has built up in the threads and prevents the fastener from threading in.
Corrosion resistance and salt spray results
If the part will be exposed to corrosive environments, the plating must resist corrosion. The vendor should provide salt spray test results if you requested them. These tests are standardized, but the results are only useful if the test conditions match your specification.
Do not rely on the plating alone for corrosion protection if the part will be in a harsh environment. The plating is a barrier. It will fail eventually. You need to understand when and how it will fail.
Red flags:
- No salt spray data for parts that will be exposed to salt, moisture, or chemicals.
- Salt spray results that do not meet the agreed acceptance criteria.
- Plating that shows rust or white rust at the edges or in scratches.
Documentation and traceability
A good plating inspection is not just about the part. It is about the record. You need to know what the part was, what it was made of, what process was used, and who made it. This is especially important for safety-critical, aerospace, or medical applications.
Check the packing list against the purchase order. Check the part numbers, quantities, and lot numbers. Check the certificate of conformance. It should state the process, the thickness, the test results, and the date. If any of this is missing, do not accept the shipment until it is provided.
Red flags:
- Missing or incomplete documentation.
- Part numbers or lot numbers that do not match the purchase order.
- Certificate of conformance that is generic and not specific to your order.
Packaging and handling
Plated parts are often more delicate than bare metal parts. The finish can be damaged during transit if it is not protected properly. Check the packaging. The parts should be separated so they do not rub against each other. They should be protected from moisture and dirt.
If the parts are in a bag, check that the bag is not cracked or torn. If they are in a box, check that the box is not crushed or wet. If the parts are in a drum or tote, check that they are not shifted or damaged.
Red flags:
- Parts rubbing against each other, which can cause scratches.
- Packaging that is wet, torn, or crushed.
- No protective layer between parts.
- Parts that are loose in the container and have shifted during transit.
A quick-reference checklist
Use this table to guide your inspection. It is not a substitute for your own procedure, but it is a good starting point.
| Check Item | What to Look For | Red Flag |
|---|---|---|
| Visual Appearance | Consistent color, no scratches, no edge burn | Dark spots, hazy finish, visible substrate |
| Thickness | Within specified range | No certificate or out-of-range thickness |
| Adhesion | Plating stays on the substrate | Flaking or peeling when lightly scratched |
| Corrosion | Salt spray results meet spec | No data or data below spec |
| Documentation | Part numbers, lot numbers, certificate match | Missing or generic documentation |
| Packaging | Parts separated, protected, no transit damage | Parts rubbing, wet or crushed packaging |
How to handle a failed inspection
If you find a defect, stop. Do not accept the part. Take photos. Note the part number, lot number, and the specific defect. Send the information to the vendor in writing. Ask for a corrective action plan. Do not just say “this is bad.” Say what is bad, how many parts are affected, and what you expect them to do.
If the vendor agrees to rework, confirm the cost and the timeline. If they do not, you may need to reject the shipment. In that case, document everything. You may need to return the parts, and the vendor may need to cover the cost.
Do not let a small defect slide. A small scratch today can become a corrosion failure tomorrow. A small thickness variation today can become a fit problem tomorrow. Be consistent in your plating inspection, and you will save money and headaches in the long run.
Final thoughts
A pre-shipment plating inspection is not a formality. It is a control. It is how you make sure the part you are accepting is the part you need. It is how you protect your production line and your end customer. It is how you keep the vendor accountable.
Use the checklist above. Adapt it to your needs. Make it part of your standard receiving process. Do it every time. The time it takes to inspect a part is small compared to the cost of a failure.
Frequently asked questions
Do I need to test every single part?
No. You can use statistical sampling, such as checking a certain number of parts per lot. For critical applications, you may need to inspect every part.
What if the vendor says the part passed but I find a defect?
Document the defect with photos and part numbers. Send the evidence to the vendor. Ask for a corrective action plan. Do not accept the part until the issue is resolved.
Can I skip the salt spray test?
Only if your application does not require corrosion resistance. If the part will be exposed to salt, moisture, or chemicals, you need the test data. Do not skip it.
How long should I keep the inspection records?
Keep them for the life of the part or as required by your industry. For aerospace, medical, or safety-critical parts, the records may be required by law.
What if the packaging is damaged but the parts are fine?
Check the parts carefully. The packaging damage may indicate that the parts were moved or exposed to moisture. Inspect them for hidden defects. If in doubt, reject the shipment.