Checklist: Verifying Anodizing Color Consistency
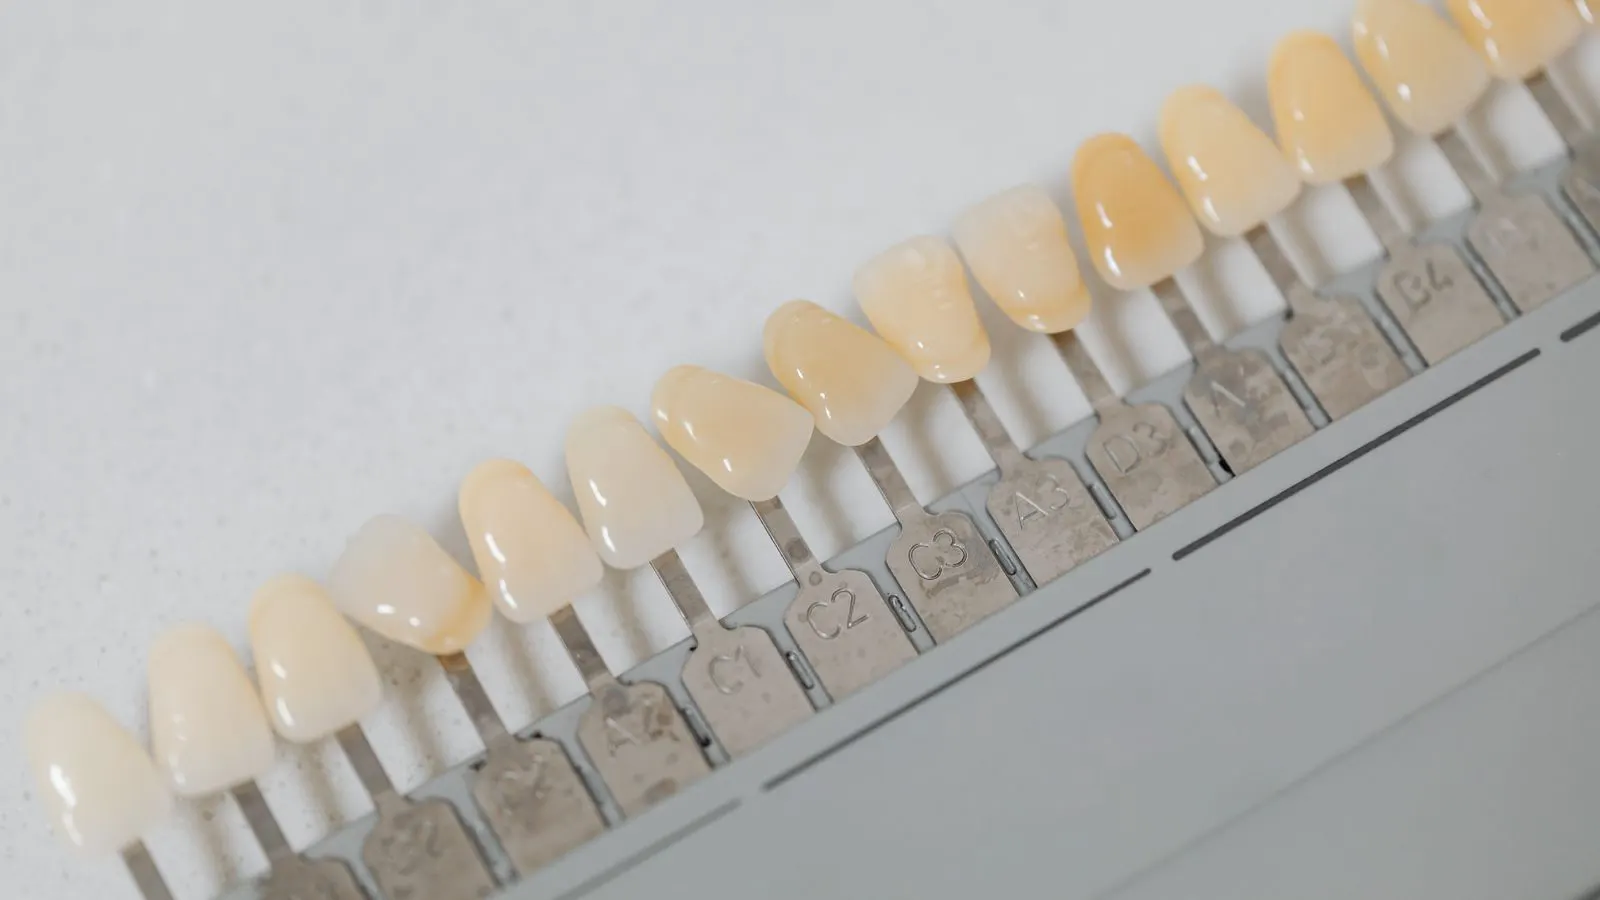
Anodizing color consistency depends on controlled dyeing, temperature management, and standardized visual comparison. Use a structured checklist to verify shade, check for defects, and confirm acceptance criteria before signing off on finished parts.
- Verify anodizing color consistency by comparing parts against approved samples under controlled lighting.
- Inspect for common anodizing defects such as streaks, pinholes, and uneven thickness that affect shade.
- Document lighting, angle, and comparison conditions during visual inspection to support repeatability.
- Track dye bath chemistry and process parameters to maintain shade stability across production runs.
- Reject parts that fail to match approved color standards even if they appear close to the naked eye.
Why Shade Drift Happens in Anodized Parts
Anodizing color consistency fails when the dyeing stage is treated as a simple finishing step rather than a controlled chemical process. The oxide layer formed on aluminum absorbs dye based on porosity, thickness, and temperature. If any variable shifts, the resulting shade changes.
A typical failure appears on a batch of anodized brackets. The first ten pieces match the approved sample. By piece twenty, the parts look slightly darker or more saturated. The cause is often a dye bath temperature drift or a change in the dwell time. The buyer receives the parts and rejects them because the shade does not match the specification.
This is why verification happens before acceptance. A structured checklist separates subjective impressions from measurable controls. The checklist below groups checks into four areas: preparation, visual comparison, defect inspection, and documentation.
Pre-Verification: Confirming the Comparison Standards
Before you place a part next to a sample, confirm that the comparison is valid. An anodized part can look different depending on the lighting source, the viewing angle, and the background surface. If the comparison conditions are wrong, the result is unreliable.
Use a set of approved color samples that have passed inspection and are stored in a stable environment. These samples should be the same material, the same finish, and the same orientation as the production parts. A sample made in a different process lot or a different dye batch can introduce its own error.
The lighting source matters. Use a light source with a stable color temperature. Many shops use a D65 light source for this purpose because it simulates standard daylight. If the shop does not specify the light source, ask. Do not compare parts under warm shop lights if the approved sample was verified under daylight simulation.
The viewing angle should be defined. Compare parts at a standard angle, usually 45 degrees from the surface. An anodized surface can appear darker at a shallow angle and lighter at a steeper angle. If the angle changes between the sample and the production part, the comparison is invalid.
The background surface should be neutral. A dark background makes light shades appear lighter. A bright background can wash out the color. Use a neutral gray or black background, depending on the shop’s standard. Keep the background consistent for every part in the batch.
Visual Inspection: Checking Shade and Uniformity
The core of color matching is visual inspection. This is where the checklist becomes practical. You are not trying to measure the exact wavelength of the dye. You are checking whether the part matches the approved sample and whether the color is uniform across the surface.
Compare the part and the sample at the same distance. Hold them at arm’s length or place them on a bench at a fixed distance. Do not bring them closer than necessary. The human eye adapts quickly to close comparison, which can mask small shade differences.
Check the entire surface, not just one area. Anodized parts can have color variation caused by porosity differences, thickness variation, or dye absorption issues. Inspect the top surface, the edges, and the recessed areas. A bracket with a flat top and a chamfered edge will show different color behavior on each feature.
Look for streaks. Streaks appear as linear bands of darker or lighter color. They are often caused by improper rinsing, a dirty dye bath, or a part that was not fully dried before dyeing. A single streak can make a part unacceptable even if the average shade is correct.
Check for pinholes. Pinholes are small dark spots where dye did not penetrate the oxide layer. They can appear as tiny dark dots on the surface. If they are concentrated in one area, the issue may be a local porosity problem or a part orientation error during dyeing.
Compare the part to the sample under the defined lighting. If the part looks correct at one angle and incorrect at another, the finish is not stable. Re-examine the part before making a decision.
Defect Inspection: Identifying Anodizing Defects
Anodizing defects directly affect color consistency. A defect that changes the oxide thickness or porosity will change how the dye is absorbed. The following defects are common in production anodizing.
| Defect | Appearance | Typical Cause |
|---|---|---|
| Streaks | Linear bands of uneven color | Incomplete rinsing, dirty dye bath, or improper drying before dyeing |
| Pinholes | Small dark spots on the surface | Local porosity variation, part orientation, or incomplete oxide formation |
| Color bleed | Blurred edges between color zones | Improper masking or dye migration during the process |
| Uneven thickness | Varying shade across the part | Current density variation or part contact with the rack |
| Etch marks | Visible lines or scratches that affect color | Surface damage before or during anodizing |
Inspect for color bleed. This occurs when dye migrates across a masked area or when the mask fails. The result is a blurred boundary between two color zones. If the part has a single color, color bleed appears as an irregular edge or a halo around a feature.
Check for uneven thickness. Anodizing thickness affects color. A thicker oxide layer absorbs more dye and appears darker. A thinner layer appears lighter. If the part shows a gradient from dark to light across the surface, the thickness is uneven. This is often caused by the part contacting the rack or by a current density problem.
Look for etch marks. If the part was scratched, dented, or exposed to an acid before anodizing, the oxide layer will not form uniformly on the damaged area. The result is a visible line or spot that does not match the surrounding color. These defects are often visible under magnification.
Do not overlook small defects. A single pinhole or a faint streak may be acceptable in a low-visibility area. It is not acceptable on a face that will be seen by the customer. The acceptance criterion depends on the part’s use. Define this before inspection.
Documentation: Recording the Verification Results
A visual inspection without documentation is a memory exercise. The next shift, or the next lot, will not know what you saw. Record the results of each check.
Create a simple inspection record. Include the part number, the lot number, the date, and the inspector’s name. Record the lighting source, the viewing angle, and the background surface. Note the approved sample reference number. This information allows another inspector to repeat the same comparison.
Record the defects found. Describe each defect by location and appearance. A note that says “streak on top surface, left corner” is more useful than “defect found.” If a defect is rejected, record the reason for rejection. If a defect is accepted, record the condition and the inspector’s approval.
Keep the approved sample with the inspection record. Do not rely on a digital photo as the sole reference. A photo can change in color depending on the monitor. A physical sample is the standard. Store the sample in a protective container away from direct sunlight.
Retain the inspection record with the shipment documentation. If the customer rejects the part later, the record shows what was checked and what was accepted. This protects both the buyer and the supplier from disputes.
Red Flags That Signal a Color Consistency Problem
Some issues appear early and point to a systemic problem in the anodizing process. Watch for these patterns.
A single part in a batch fails the color check. This is often an isolated defect. The part may have been oriented incorrectly, or the dye may have been applied unevenly to one area. Reject the part and continue the inspection.
Multiple parts in a batch fail the same way. If five parts all have streaks in the same direction, the problem is likely in the rinse or the dye bath. Do not continue the inspection as if each part is independent. Stop and report the issue to the supplier.
The approved sample does not match the production part under different lighting. If the sample looks correct under D65 lighting but wrong under shop lights, the finish is not stable. The dye may be too sensitive to lighting conditions. Ask the supplier to re-verify the sample under the same lighting you will use.
The color changes over time. If you store the approved sample and it looks different after a week, the sample is not stable. This can happen if the sample was exposed to moisture, heat, or UV light. Request a new approved sample and re-verify the production part.
The shade varies between batches. If batch one matches the sample and batch two is darker, the dye bath chemistry has shifted. The supplier should be able to explain the change. If they cannot, the process is not controlled.
Final Acceptance Decision
The final decision is a yes or no. The part either meets the color specification or it does not. Do not accept a part that is “close enough” unless the specification allows for a tolerance. Anodizing color is not binary. It exists on a spectrum. The approved sample defines the target. The part must match that target.
If the part passes all checks, sign off on the inspection record. If it fails, return it to the supplier with the record. Include the lighting, angle, and defect details. A clear rejection note reduces the time to resolve the issue.
Do not allow a single inspector to be the only gate. A second inspection is useful for high-value parts or for a new supplier. The second inspector should use the same conditions and the same sample. If the two inspectors disagree, re-examine the part and the sample. Do not rely on a third opinion without re-verification.
Color consistency is a control problem. It is solved by defining the standard, checking the conditions, inspecting for defects, and documenting the result. The checklist in this article provides that structure. Use it for every batch. Do not skip a step because the part looks right. The next batch may not.
Common Questions About Anodizing Color Consistency
Q: Can I use a color meter to verify anodizing color consistency?
A: A color meter can provide a numerical reference, but visual comparison against an approved sample is the standard acceptance method. The meter is useful for tracking drift across lots, not for final visual acceptance.
Q: How do I handle a part that is the correct shade but has a small streak?
A: Reject the part if the streak is visible under the defined lighting and viewing angle. If the streak is only visible under magnification and the specification does not require it, document the acceptance and move on.
Q: What if the approved sample was made in a different dye lot than the production part?
A: Request a new approved sample made from the same dye lot and process conditions. Do not use the old sample as the reference. A dye lot change can shift the shade even if the process is identical.
Q: Should I compare parts under natural daylight?
A: Natural daylight is not stable. It changes with time of day, weather, and season. Use a controlled D65 light source for consistent results. Natural daylight is acceptable for a quick check but not for final acceptance.
Q: How often should I re-verify the approved sample?
A: Re-verify the sample at the start of each production run and after any storage period longer than a few weeks. If the sample has been exposed to moisture, heat, or UV light, replace it with a new one.
===END===


